How to Choose the Right Precision Casting Supplier?
Choosing the right Precision Casting supplier can shape your product’s quality, cost, and delivery performance. It is not simply a search for the lowest quotation. A capable partner should understand alloy behavior, mold design, shrinkage control, heat treatment, and machining allowances. These details often decide whether a part fits correctly after production.
Practical evaluation begins with evidence. Ask for material certificates, dimensional inspection reports, process-control records, and representative samples. Review the supplier’s foundry equipment, testing capabilities, and experience with similar components. A reliable manufacturer should explain how it manages porosity, surface defects, tolerance variation, and batch traceability. It should also communicate clearly when a drawing needs improvement. That honesty matters.
Look beyond the first sample.
Price still matters, but it should be compared with tooling life, rejection rates, packaging, logistics, and revision costs. A supplier with strong quality systems, qualified personnel, and consistent inspection methods may reduce long-term risk. Certifications can support credibility, but certificates alone do not prove daily performance. Verify their scope, validity, and practical application.
No supplier is perfect. That assumption deserves scrutiny. Even experienced teams can underestimate a difficult geometry or a demanding alloy. The strongest selection process leaves room for technical questions, trial production, and measurable correction. Before signing an agreement, define acceptance criteria, reporting requirements, delivery expectations, and responsibilities for changes. With careful verification, buyers can choose a Precision Casting partner that supports dependable production rather than creating avoidable surprises.
Define Your Precision Casting Requirements and Quality Standards
Choosing a precision casting supplier starts with a clear requirement sheet, not a sales presentation.
Define the alloy grade, casting weight, wall thickness, dimensional tolerances, surface finish, and annual volume. State critical features clearly, such as a 1.5 mm passage or a sealing face requiring 0.05 mm flatness. Also specify inspection methods, including coordinate measuring, radiography, or CT scanning. The World Foundry Organization’s 2023 census reported global casting production above 100 million tonnes in 2022. That scale makes process control essential, even for small components.
Quality standards must be measurable and traceable.
Request material certificates, heat-lot identification, inspection records, and corrective-action reports. ISO’s 2022 Survey recorded more than 1.2 million ISO 9001 certificates worldwide. Certification supports confidence, but it does not replace product evidence. Ask how the supplier controls shrinkage, porosity, tooling wear, and first-article approval. In my experience, teams sometimes over-specify cosmetic requirements while missing functional tolerances. That mistake increases cost without improving performance. A perfect-looking checklist can still be incomplete.
Tips:
Give suppliers a controlled drawing revision and a sample part. Separate critical, major, and minor characteristics. Agree on acceptance limits before production begins. Ask for process capability data, not only final inspection results. Review a real inspection report with the supplier’s engineer. If a supplier cannot explain where defects may occur, pause before approving the order. Some requirements may need revision after a trial casting; that is normal, and ignoring the lesson is not.
Verify Certifications, Quality Control, and Inspection Processes
A precision casting supplier should prove quality through records, not polished promises. A certificate is evidence, not proof.
Start by checking the certificate number, issuing body, covered site, and expiration date. Confirm the scope includes casting, heat treatment, and inspection activities. The 2023 ISO Survey recorded 1,265,216 ISO 9001 certificates worldwide. That number shows certification is common, not automatically distinctive. Ask how the supplier controls alloys, wax patterns, ceramic shells, furnace settings, and rework. Each heat should link to a material certificate and production batch. Missing traceability is a serious warning.
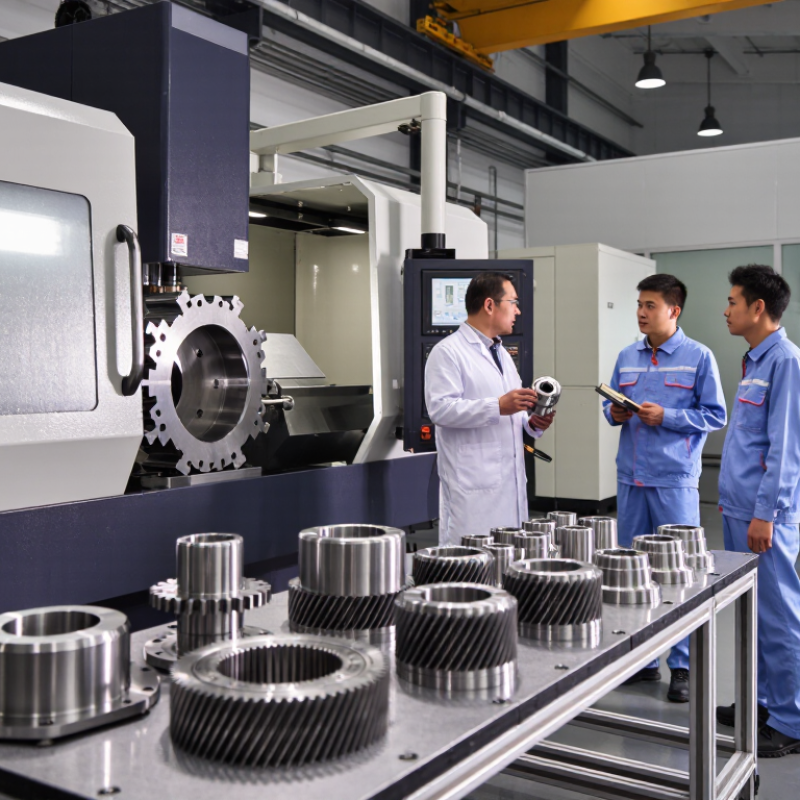
Quality control must continue beyond visual inspection. Request sample inspection plans, process capability studies, and nonconformance reports. Useful evidence includes spectrometer results, dimensional reports, tensile data, and penetrant or radiographic testing. Measurements should identify equipment, calibration status, operator, and acceptance criteria. ASTM International’s 2023 annual report referenced more than 12,000 consensus standards. Ask the supplier to state the exact standard and revision used for each test. Vague references create avoidable disputes. During an audit, compare the report with the actual shop floor. The gauge may be calibrated, but the operator may still record the wrong feature. That uncomfortable gap deserves attention. Also review corrective-action records. A supplier hiding every defect may be less reliable than one documenting and fixing them.
How to Choose the Right Precision Casting Supplier?
Recommended evaluation weighting for certifications, quality control, and inspection processes
Quality control and inspection capability receive the highest weighting because they directly affect dimensional accuracy, defect prevention, and batch-to-batch consistency. Verify applicable certifications such as ISO 9001, review documented process controls, and confirm that inspection equipment is calibrated and traceable.
Compare Costs, Lead Times, Communication, and Customer Support
Choosing the right precision casting supplier requires more than comparing unit prices. Cost deserves a detailed review. Request an itemized quotation covering tooling, inspection, packaging, freight, and revision charges. A low casting price can hide expensive tooling or unclear tolerance requirements. Ask whether the quote includes material certificates and dimensional reports. In my experience, unclear quotation terms create disputes later. I once accepted a cheaper offer and paid extra for repeated drawing changes. That decision was avoidable.
Lead time should show each production milestone, not only a final delivery date. Ask for schedules covering pattern making, sample approval, casting, machining, inspection, and packing. A supplier promising ten days may not have checked its current capacity. Confirm available equipment and planned production slots. Use written milestones. Request prompt notice when risks appear. Still, estimates can slip. Material shortages, equipment repairs, and late approvals may affect delivery. I prefer a realistic date with visible assumptions over an impressive promise.
Communication reveals operational discipline. During technical reviews, notice whether engineers ask precise questions about wall thickness, draft angles, and critical surfaces. A dependable team records decisions and sends updated drawings quickly. Ask who will manage your project and how support works after delivery. Request inspection reports, corrective-action records, and a clear response time for complaints. These documents improve traceability. One weakness deserves attention: some suppliers communicate well before payment, then respond slowly afterward. That silence creates production uncertainty, especially when a rejected batch sits beside your receiving dock.
How to Choose the Right Precision Casting Supplier? - Compare Costs, Lead Times, Communication, and Customer Support
| Evaluation Criterion |
Supplier Profile A |
Supplier Profile B |
Supplier Profile C |
Supplier Profile D |
| Typical order volume |
Prototype to 500 parts |
500–5,000 parts |
5,000–50,000 parts |
1,000–20,000 parts |
| Indicative tooling cost |
US$800–2,500 |
US$1,500–4,000 |
US$3,000–8,000 |
US$2,000–5,500 |
| Estimated unit price at 1,000 parts |
US$18–32 |
US$14–26 |
US$11–22 |
US$16–29 |
| Prototype lead time |
10–15 business days |
15–20 business days |
20–30 business days |
12–18 business days |
| Production lead time |
20–30 business days |
25–40 business days |
35–55 business days |
25–45 business days |
| Material options |
Common stainless steel, carbon steel, and aluminum alloys |
Steel, stainless steel, nickel alloys, and selected aluminum alloys |
Broad alloy range, including heat-resistant and corrosion-resistant grades |
Common engineering alloys with limited special-alloy capacity |
| Dimensional capability |
Approximately CT6–CT8 for suitable geometries |
Approximately CT6–CT8 with process approval |
Approximately CT5–CT7 for controlled production runs |
Approximately CT7–CT9 for standard applications |
| Quality documentation |
Certificate of conformity and basic inspection report |
Material certificates, dimensional reports, and batch traceability |
Full inspection plan, material traceability, process records, and first-article documentation |
Material certificates and dimensional inspection available at additional cost |
| Communication response time |
Usually within 1 business day |
Usually within 1–2 business days |
Usually within 2–3 business days |
Usually within 1–2 business days |
| Engineering support |
Basic design-for-casting feedback and drawing review |
Detailed manufacturability review and process recommendations |
Advanced simulation, tooling optimization, and root-cause analysis |
Drawing review with limited simulation capability |
| Customer support |
Dedicated contact for quotations and order updates |
Project coordinator plus scheduled production updates |
Dedicated project team, formal escalation process, and after-sales review |
Shared support contact with periodic order updates |
| Best suited for |
Fast prototypes and low-volume custom parts |
Balanced cost, quality, and moderate production volume |
High-volume or highly regulated applications |
Cost-sensitive standard components |
| Overall suitability score |
3.9 / 5 |
4.4 / 5 |
4.6 / 5 |
3.7 / 5 |
Note: Cost and lead-time ranges are illustrative industry benchmarks for comparable precision-casting projects. Actual quotations depend on part geometry, alloy, weight, tolerances, finishing requirements, order quantity, inspection level, and shipping destination.
Assess Samples, References, and Long-Term Supplier Reliability
Choosing a precision casting supplier requires more than comparing prices. Start by examining physical samples under strong, neutral lighting. Check wall consistency, edge definition, surface texture, and machining allowance. Ask for dimensional reports linked to the exact sample. A polished sample proves little alone. Request a sectioned piece when internal porosity matters. Review the alloy certificate, inspection method, and heat-treatment record. These documents reveal whether quality is measured or simply claimed.
References should come from customers with similar alloys, tolerances, production volumes, and delivery pressure. Ask specific questions: Did the supplier solve recurring defects? Were corrective actions documented? How often did shipments arrive late? A reference call should include an engineer, not only a salesperson. If possible, visit the foundry and observe pattern control, wax handling, shell storage, and final inspection. Small details matter. Clean records matter too. Still, one visit can create false confidence; a tidy production day is not the whole process.
Long-term reliability appears in repeatability. Request capability data from several production lots, not one carefully selected batch. Review nonconformance trends, response times, tooling ownership, and backup plans for equipment or material shortages. A dependable supplier explains bad results without defensiveness and shares a dated recovery plan. Test communication before signing: send a technical question and assess the clarity of the reply. Keep a written scorecard for samples, references, quality systems, and delivery history. In practice, vague answers become expensive later. Leave room for doubt, and verify critical claims independently.